
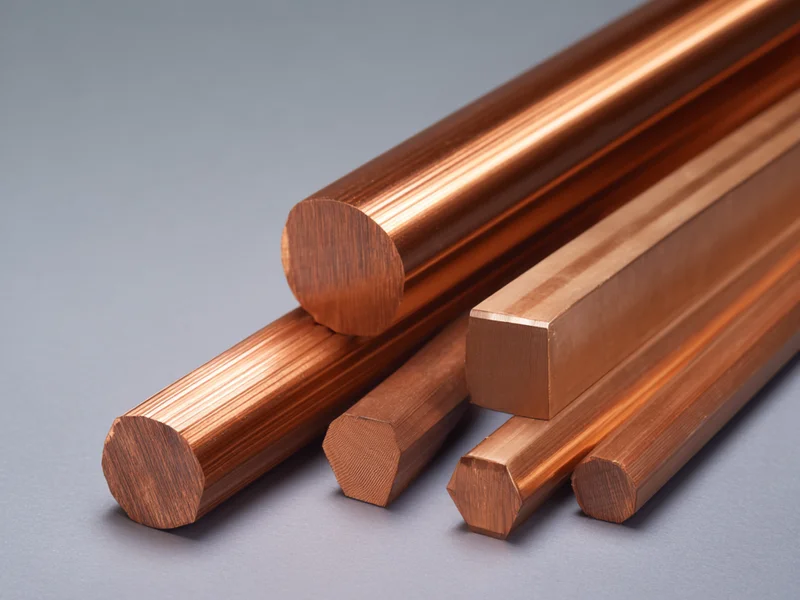
RWMA Class 1 Copper Zirconium (C15000) has the highest conductivity among the Class 1-4 copper alloys for resistance welding. With a minimum conductivity of 80% IACS per AWS J1.3, this material is the preferred choice when maximum heat dissipation and minimal interaction with metallic coatings are required, especially zinc on galvanized steels.
The controlled addition of 0.10-0.20% zirconium (Zr) provides the precipitation hardening needed to maintain useful hardness (≥65 HRB) without significantly sacrificing conductivity. This unique combination makes C15000 the ideal material for applications where other electrodes suffer from sticking, build-up or premature wear caused by alloying with zinc.
AWS J1.3 Technical Specifications
| Property | Value | Unit |
|---|---|---|
| UNS Designation | C15000 | - |
| Composition | Cu + 0.10-0.20% Zr | % wt |
| Electrical Conductivity | ≥80 | % IACS (AWS J1.3) |
| Hardness | ≥65 | HRB (AWS J1.3 min, round rod up to 1") |
| Thermal Conductivity | 365 | W/m·K (typical) |
| Softening Temperature | 525 | °C (typical) |
| Tensile Strength | 410-520 | MPa (typical, rod up to 1") |
Recommended Applications
The Zinc Problem and the Class 1 Solution
When welding galvanized steels, the zinc coating melts at ~420°C and tends to alloy with the copper of the electrode, forming brass (CuZn). This phenomenon causes:
- Sticking of the electrode to the workpiece
- Build-up of material on the electrode face
- Accelerated wear and loss of geometry
- Inconsistency in nugget quality
The high conductivity of Class 1 dissipates heat more rapidly, keeping the electrode face temperature below the alloying point of zinc with copper.
When NOT to Use Class 1 (and What to Use Instead)
Class 1 is not the "basic" option — it's a specialized material and typically more expensive than Class 2.
❌ Don't use Class 1 if:
- You're experiencing rapid wear — Class 1 has lower typical hardness than Class 2 (depending on thermal conditions). If you're changing electrodes frequently due to wear, the problem is hardness.
- You're not working with galvanized or coated materials — High conductivity (≥80% IACS) only pays off when there's zinc, Al-Si, or other coatings causing sticking.
- Your process doesn't use low current — If you're using high currents on normal steel, Class 1 provides no advantage and you're overpaying.
- You're looking for the most economical option — Class 1 costs more than Class 2. If you don't have sticking problems, you're overpaying.
📋 Plant examples:
- Automotive galvanized + sticking → Yes, use Class 1. Better conductivity → less heat needed → less zinc alloying. Tip: adjust up-slope parameter before changing material.
- Automotive caps (e.g. LUVATA) → Class 1 is the standard. Well-tuned machines + low current + low pressure = best results.
- Uncoated steel + wear → Don't use Class 1. Use Class 2 or Class 3 for higher hardness.
✓ Use this instead:
- Class 2 (C18200/C18150) — Higher hardness, more economical, the standard for ~80% of steel applications.
- Class 3 (C17510/C18000) — If you also have UHSS, high pressure, or projection welding on top of wear issues.
⚡ Quick Checklist (30 sec):
Quick rule: Class 1 is for galvanized + sticking + low current. If you don't have that combination, Class 2 is probably the better choice.
Tell me: material, thickness, coating, and welder type, and I'll recommend the exact class.
Request technical recommendation →What We See in Real Applications
In automotive plants working with galvanized materials and medium frequency:
- Automotive caps: Brands like LUVATA use Class 1 in their caps. The key: well-tuned machines running at the lowest current and pressure possible.
- Why does it work? Lower pressure = more heat in the weld zone. Lower current = machine in good order. Class 1 conducts better, so it needs less heat to weld.
- Key parameter - Up-slope: Before changing material, adjust the up-slope. Many times sticking problems are solved with parameters, not material changes.
If you're not sure which material is right for your application, let's review it together before quoting.