
Elkonite Copper-Tungsten (CuW) Sales in Mexico
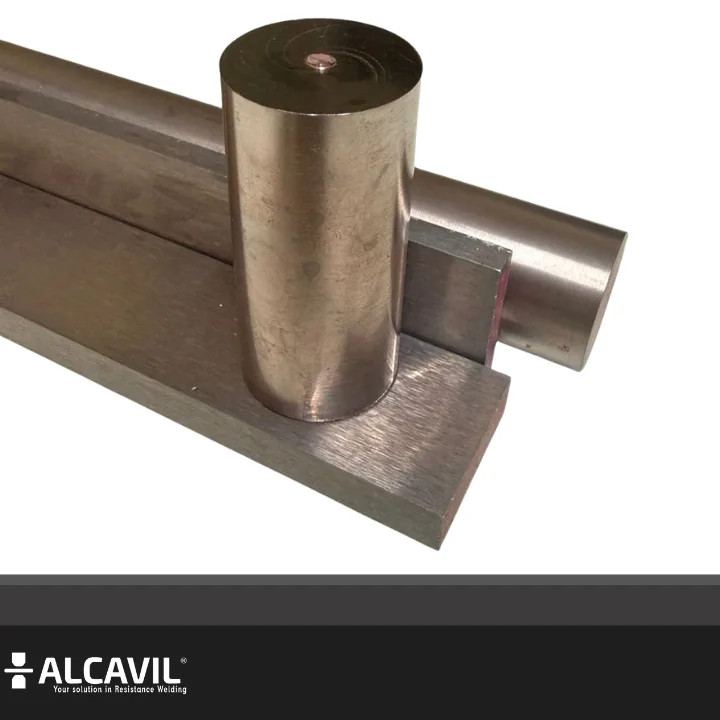
Copper-tungsten composite for high thermal demand applications. The industry standard for nut projection welding, die facings and faced electrodes where copper alloys don't hold up.
Applicable standards: AWS J1.3 • RWMA Class 10, 11, 12
ALCAVIL is a leading supplier of Elkonite Copper-Tungsten (CuW). Classes 10, 11 and 12 for nut and stud projection welding. Permanent stock in Monterrey. Request quote →
Available Grades by RWMA Class
Higher tungsten content means higher hardness and wear resistance, but lower conductivity. Select based on your application severity.
The RWMA classification system divides Copper-Tungsten materials into three classes according to their tungsten content: Class 10 with approximately 55% tungsten for standard projection applications, Class 11 with 73-77% tungsten, the most versatile and widely used grade in the industry, and Class 12 with 78-82% tungsten for the most severe applications where maximum wear resistance is required. Correct grade selection directly impacts electrode life and weld quality.
Elkonite® 5W3
Standard ProjectionElkonite® 10W3
Most UsedWhen to use Elkonite vs Copper Alloys?
Use Copper-Tungsten when copper alloys (Class 2 or 3) wear quickly or deform from temperature. Typical cases: nut projection on steel, high volume production (>1000 pieces/day), or when the electrode can't cool adequately between cycles.
Note on Trademarks and RWMA Classification
Elkonite® is a registered trademark of CMW Inc. (formerly Contact Metal Welding). Similar to how "Kleenex" became synonymous with facial tissues, "Elkonite" has become the generic name for Copper-Tungsten composites in the resistance welding industry. It is also misspelled as elconite, elkon or elkomet — all refer to the same copper-tungsten (CuW) material, RWMA Classes 10-12. Values shown are typical manufacturer values, not AWS J1.3 minimums. AWS specifies composition ranges: Class 10 (43-47% Cu), Class 11 (23-27% Cu), Class 12 (18-22% Cu). By composition, 1W3 corresponds to Class 10; 3W3 and 5W3 fall between Class 10 and Class 11.
Looking for ready-machined electrodes? We manufacture tungsten and molybdenum insert electrodes ready to use. Includes Morse tapers 1 and 2, EDM machining, and mirror finish available in molybdenum.
When NOT to Use Elkonite/CuW (and What to Use Instead)
Elkonite is the most expensive material — only use it when truly justified.
❌ Don't use Elkonite/CuW if:
- Class 3 already works well for you — If your Class 3 electrodes have good life in projection, don't spend more.
- It's standard spot welding — For spot welds, copper alloys (Class 2 or 3) are more suitable. CuW is for projection and inserts.
- The problem is setup, not wear — Elkonite won't fix misconfigured parameters or misalignment. Validate your process first.
- The electrode DEFORMS, doesn't wear — If it's getting "crushed" instead of losing material, it's a parameter or pressure issue, not material.
📋 Plant Examples:
- M8 projection with C17510, electrodes last 800 welds → Acceptable life. Elkonite would be over-engineering. Continue with Class 3.
- M10 projection with Class 3, electrodes last only 200 welds and look worn → That DOES justify Elkonite 10W3. Tungsten resists abrasive wear better.
✓ Use this instead:
- Class 3 (C17510/C18000) — If you have moderate wear in projection but C3 still works.
- Class 2 (C18200) — If it's standard spot welding on steel.
⚡ 30-Second Checklist:
- □ Does Class 3 last less than 300 welds in projection? → Consider Elkonite
- □ Is it normal spot welding? → You DON'T need Elkonite
- □ Does the electrode crush/deform? → Check parameters first
Not sure if Elkonite is worth it for your application? Tell us your current electrode life and we'll help you decide if the upgrade is justified →
What We See in Real Applications
- 10W3 (Class 11) is the standard: It's what we use most for nut and stud projection. The 75% tungsten / 25% copper balance works well for most applications.
- 30W3 (Class 12) for contacts: With 80% tungsten, it's used more for conductive components like electrical terminals than for welding.
- 5W3 is rare: In our experience, it's rarely used - most applications work better with 10W3.
- Wear vs deformation: If your electrode wears (loses material), Elkonite helps. If it deforms (gets crushed), it may be a parameter issue.
If you're unsure which grade you need, 10W3 is the recommended starting point for projection. See how the insert is brazed and mounted in projection welding electrodes and tooling.
Comparison Table - Elkonite® Family
The following table presents the physical and mechanical properties of all available Copper-Tungsten grades. Electrical conductivity values are expressed as a percentage of the International Annealed Copper Standard (IACS). Note that the highlighted grades are the ones we stock.
| RWMA Class | Grade | Composition | % IACS | Hardness | Density |
|---|---|---|---|---|---|
| Class 10 | 1W3 | 45% Cu / 55% W | 53 | 79 HRB | 12.6 g/cm³ |
| — | 3W3 | 32% Cu / 68% W | 50 | 88 HRB | 13.93 g/cm³ |
| — | 5W3 | 30% Cu / 70% W | 48 | 90 HRB | 14.18 g/cm³ |
| Class 11 | 10W3 | 25% Cu / 75% W | 46 | 98 HRB | 14.70 g/cm³ |
| Class 12 | 20W3 | 22% Cu / 78% W | 44 | 99 HRB | 14.80 g/cm³ |
| Class 12 | 30W3 | 20% Cu / 80% W | 42 | 103 HRB | 15.4 g/cm³ |
Need the finished electrode or insert? We don't just sell the material: we manufacture resistance welding electrodes with Elkonite 10W3, 5W3 and 30W3 inserts, including projection welding electrodes for nuts and studs.