
Refractory Metal Faced Electrodes · RWMA Class 13 and 14
Tungsten and Molybdenum Insert Electrodes
Refractory material electrodes for welding copper terminals, silver contacts and electrical components. Precision EDM machining and certified metrology.
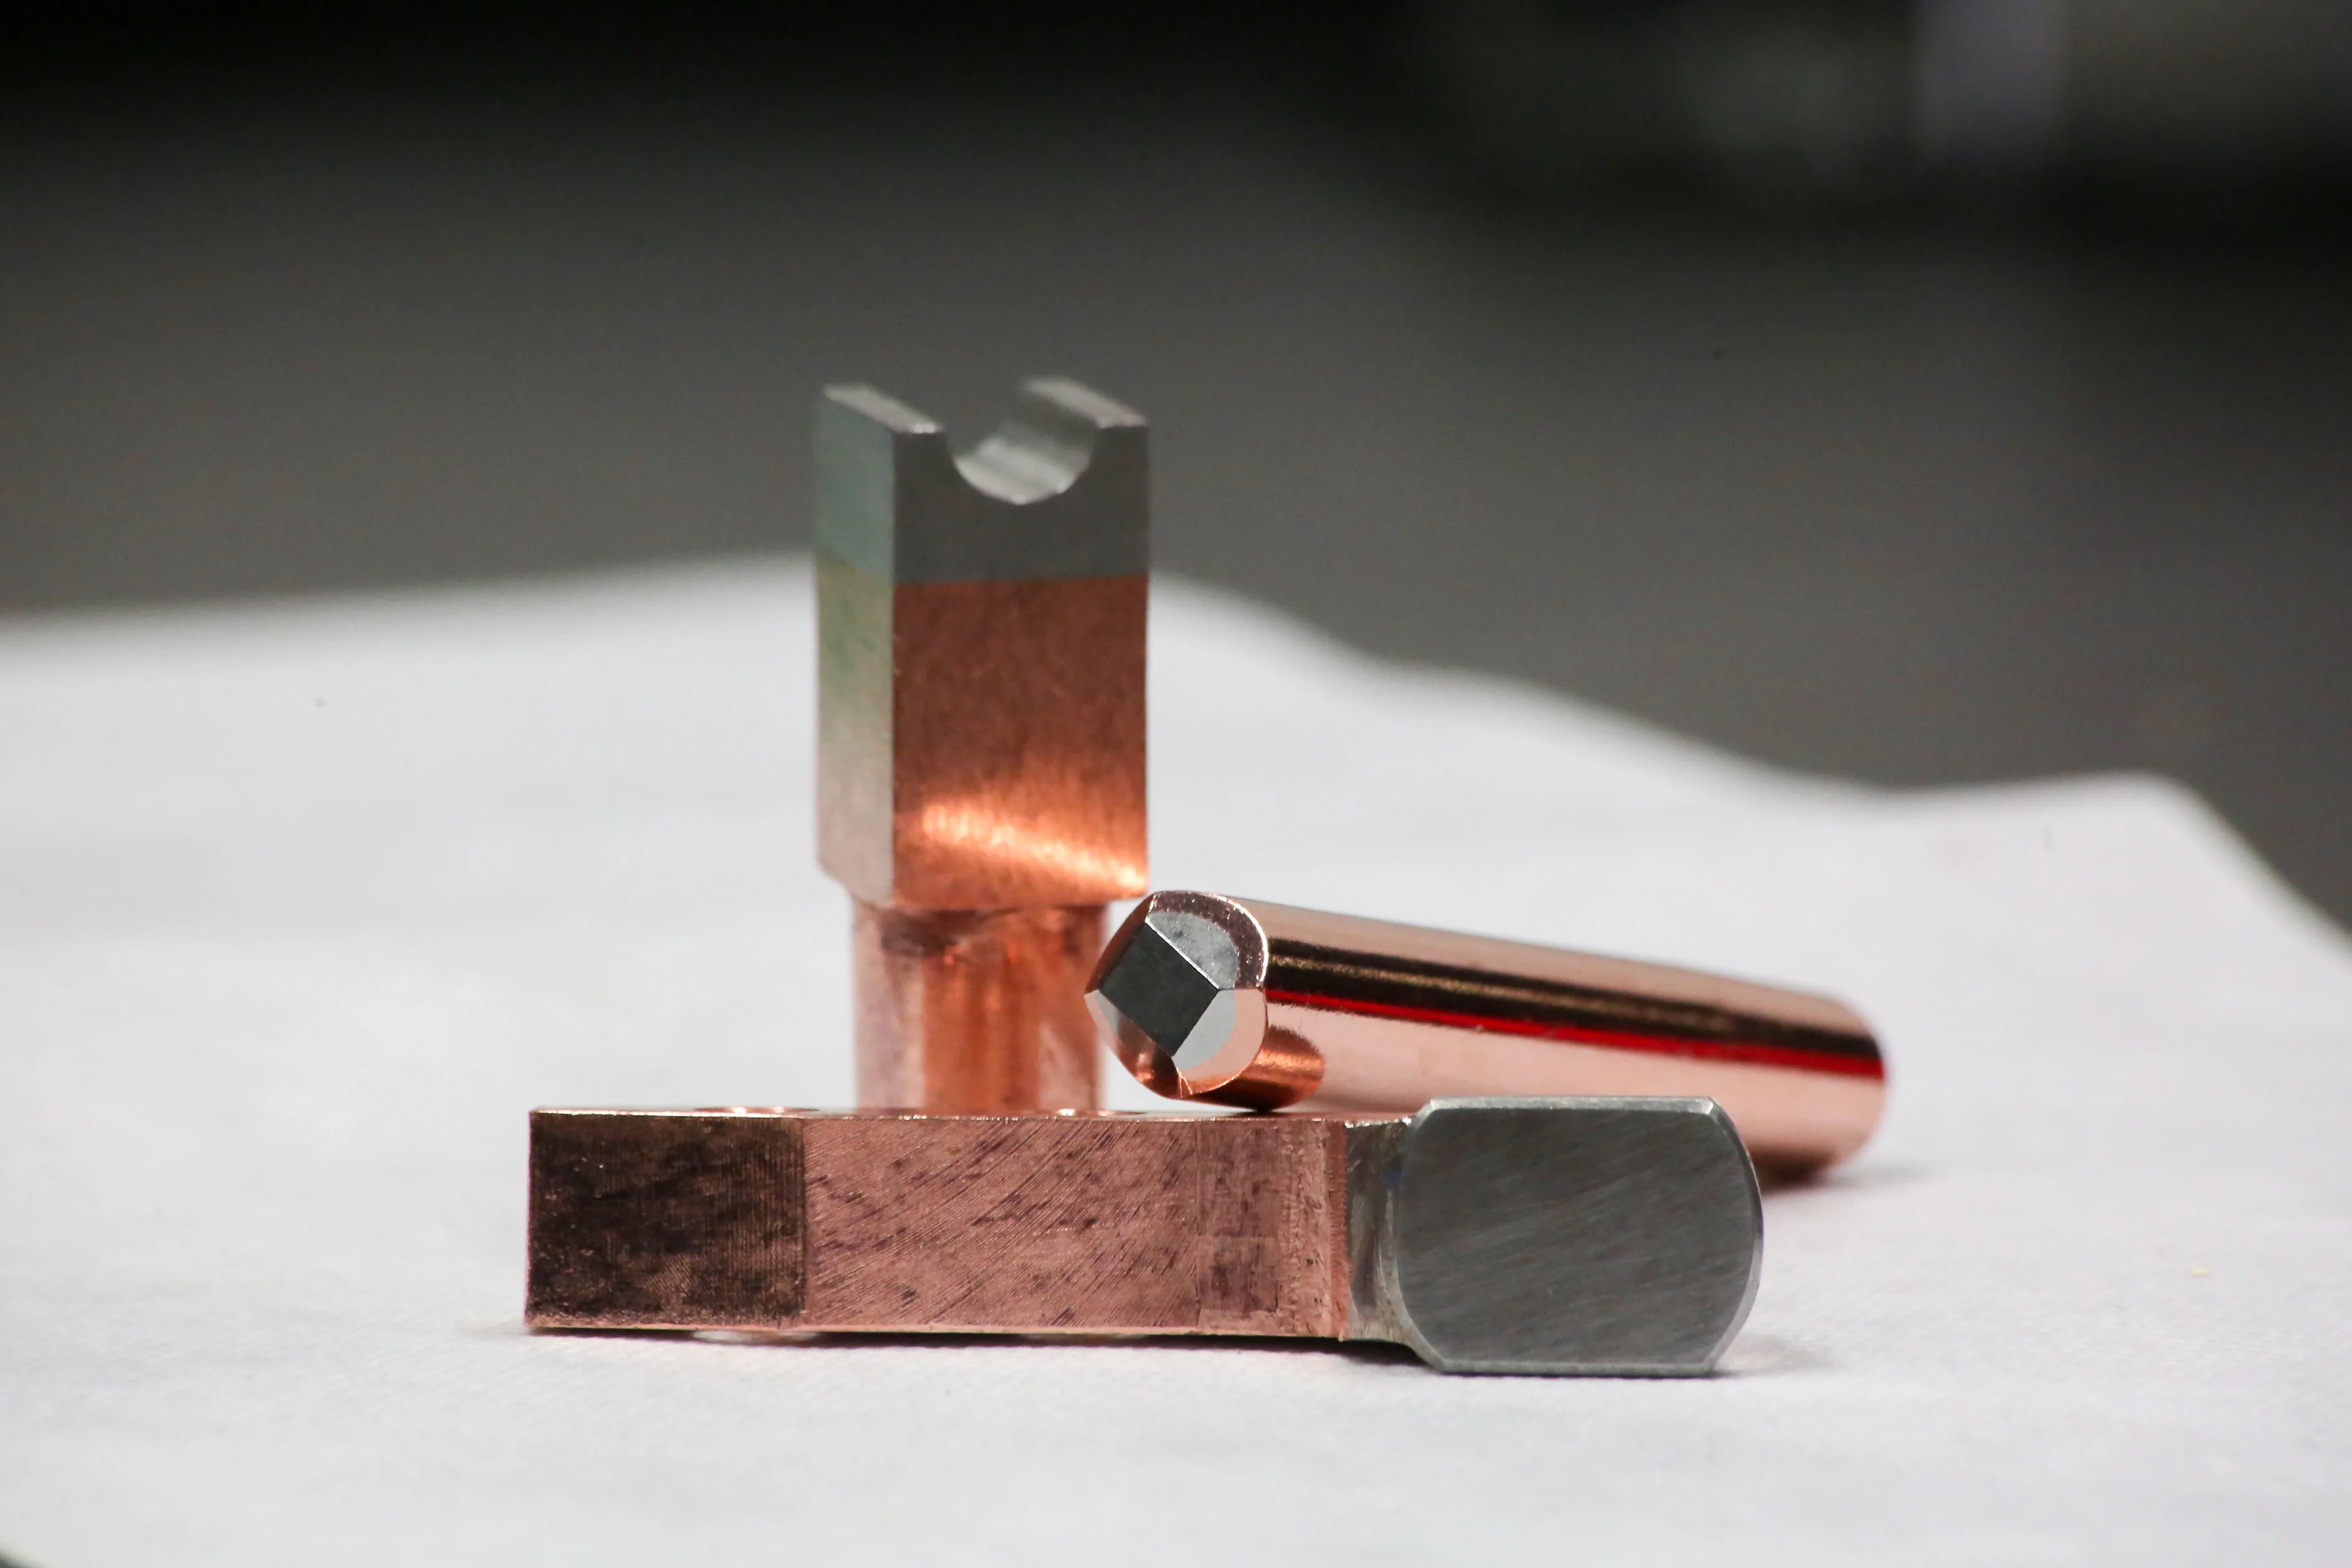
Our tungsten insert electrodes and molybdenum insert electrodes are manufactured with a tip of refractory material (W or Mo) inserted into a Class 2 copper body. They are the ideal solution for those looking for tungsten electrodes for resistance welding of electrical contacts, copper terminals and silver components. Tungsten (RWMA Class 13) offers the highest melting point of all metals (3,422°C), although it is a brittle material; molybdenum (RWMA Class 14) is more machinable and allows a mirror finish for maximum-precision applications.
What are Insert Electrodes?
Refractory Metal Faced Electrodes are specialized electrodes that use tungsten (RWMA Class 13) or molybdenum (RWMA Class 14) at the contact face. These materials have extremely high melting points and do not stick to molten copper.
They are essential for electrical contact welding, copper terminals, contactors, switches and electrical switchgear. Typical customers include manufacturers like Siemens, Schneider Electric, Phoenix Contact and BorgWarner.
Available Products
- Tungsten Electrodes (W, WLa10, WLa15, WLa20) Pure and lanthanated tungsten for copper terminals in motors and electrical components. Higher hardness and wear resistance. WLa15 and WLa20 recommended for 24/7 production.
- Molybdenum / TZM Electrodes Mirror finish available for silver contacts without marks. TZM (Ti-Zr-Mo) for higher high-temperature resistance. More economical than tungsten with excellent performance.
- Elkonite (CuW) Electrodes Copper-Tungsten for precise parameter control in special applications. Combines copper conductivity with tungsten hardness.
- Morse Taper 1 and Morse 2 Standard mounting for electrical contact welding equipment. Taper size depends on the equipment design and the electrode cavity.
Mirror Finish on Molybdenum Electrodes

The mirror finish is a complex process that requires a specialized combination of polishing products and techniques. At ALCAVIL we have mastered this process over years of experience. The result is a surface so smooth that it reflects objects like a mirror, eliminating any marks on the welded silver contacts.
Tungsten vs Molybdenum: Key Differences
Both materials have the same electrical conductivity (approximately 30% IACS), but very different characteristics:
- Tungsten: Highest melting point of all metals (3,422°C). It is brittle and only allows an improved roughness finish, not mirror.
- Molybdenum: Lower melting point (2,623°C) but more machinable. Allows a mirror finish for silver contacts without marks.
Video: Mirror finish reflecting a pen - ALCAVIL surface quality
Technical Differentiator – AWS J1.3
Micrometric Precision: Our Class 13 tungsten and Class 14 molybdenum electrodes are manufactured with EDM machining to avoid fractures in the brittle material. Mirror finish on molybdenum eliminates marks on silver contacts. High-precision metrology equipment verifies tolerances on each part.
Need Specifications or Pricing?
Get technical data sheets or a custom quote for your insert electrode requirements.
Manufacturing Capabilities
EDM Machining
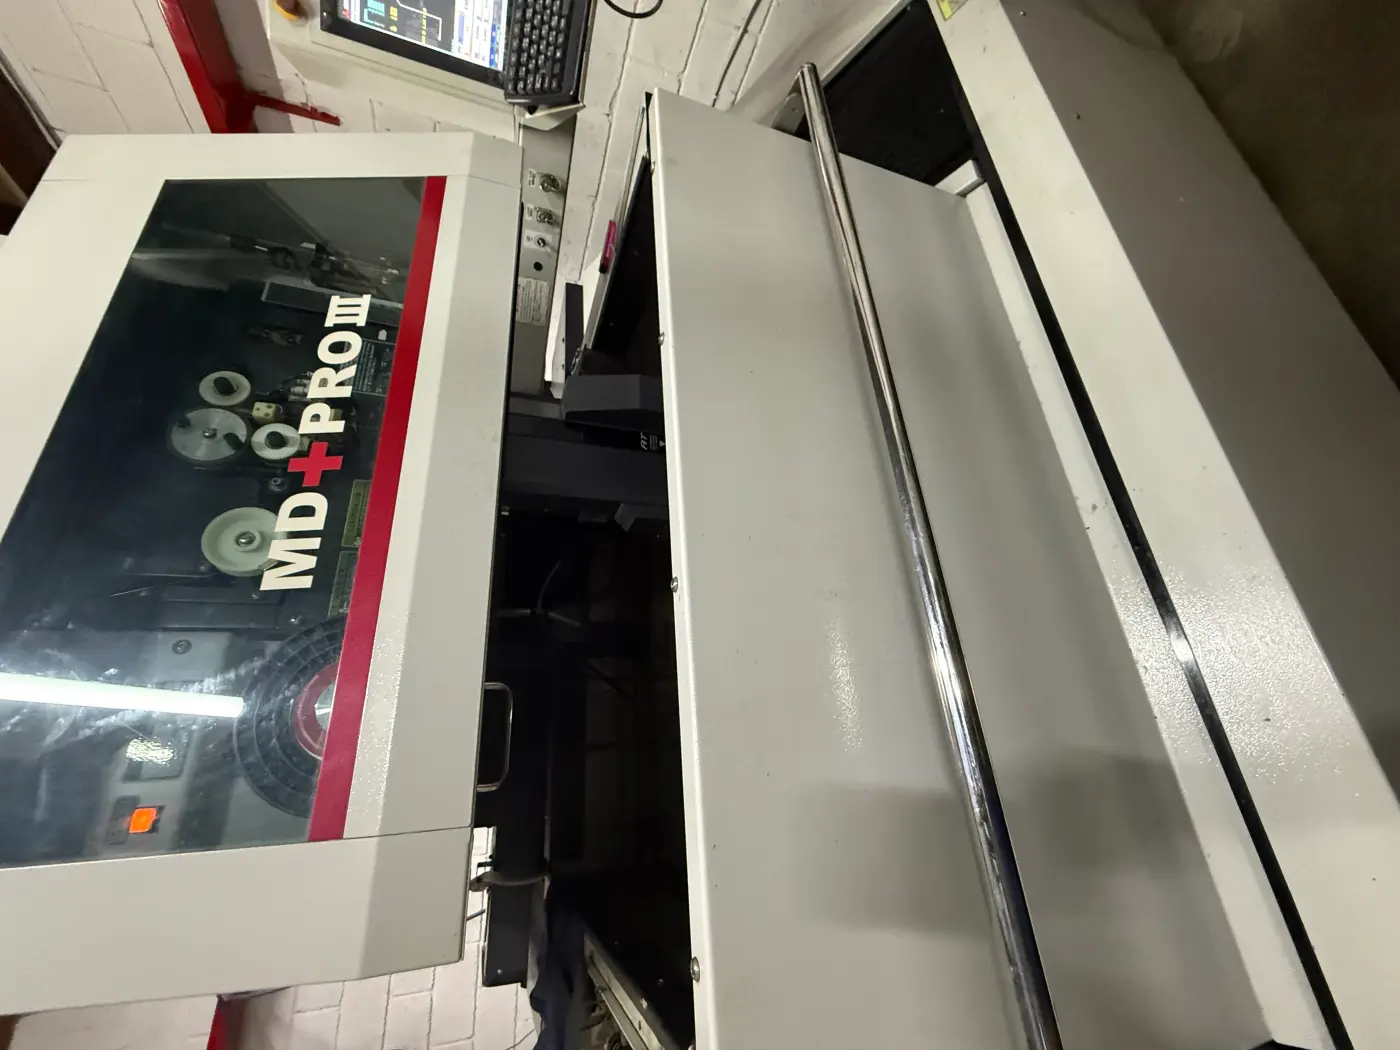
Precision electrical discharge machining for tungsten. The material is brittle and requires EDM cutting to avoid fractures and achieve tight tolerances.
Computerized Metrology
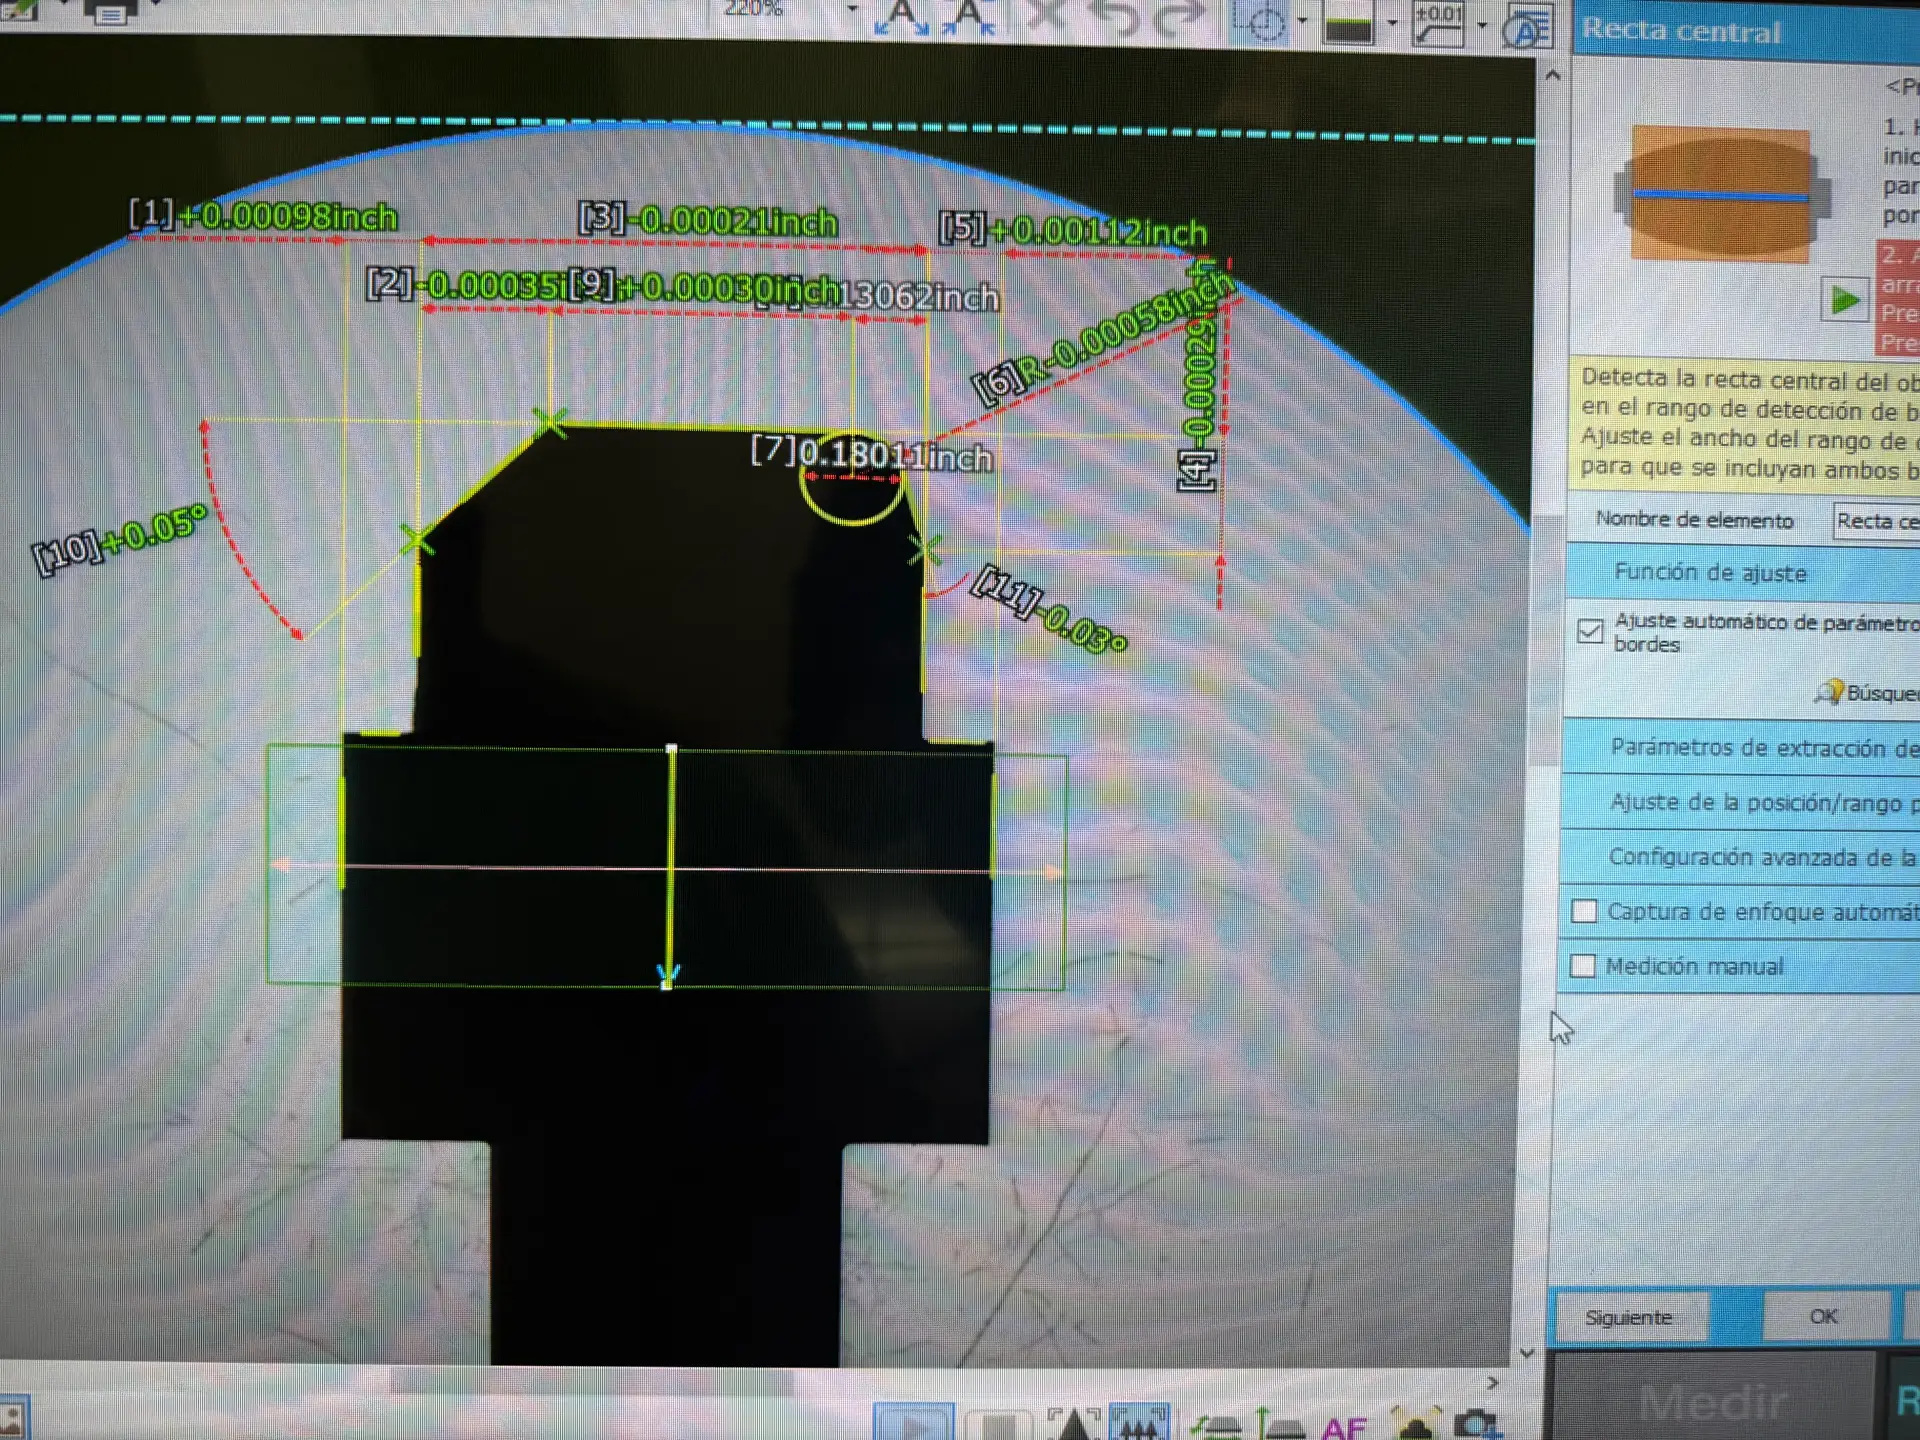
High-precision optical measurement system to verify dimensions and tolerances on each manufactured electrode.
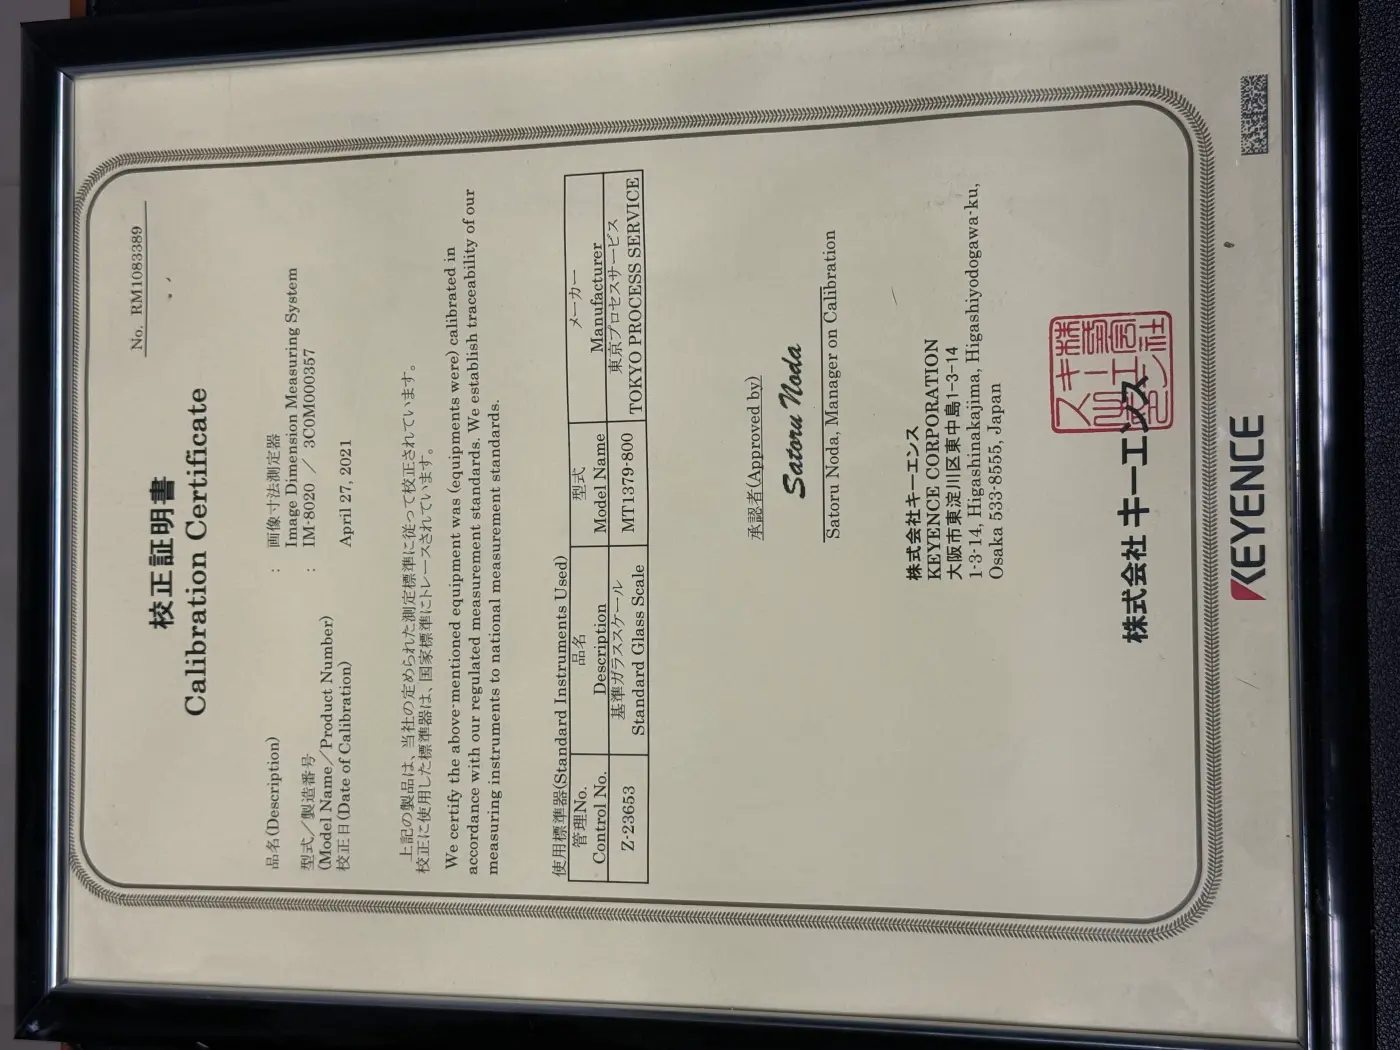
Certified Equipment
Our measuring equipment has current calibration certificates that guarantee the precision of each part.
Applications
- Copper Terminals Terminal welding in electric motors, automotive harnesses and power components.
- Silver Contacts Contact joining in relays, contactors and switches. Mirror finish on Mo for zero marks.
- Switches and Switchgear Switchgear and medium/low voltage electrical distribution components.
- Electronic Components Precision welding in power electronics and industrial control components.
Tungsten Types
We offer pure and lanthanated tungsten per ISO 6848:
- WP (Green) - Pure Tungsten 99.95% For low-volume basic applications. Economical but shorter service life.
- WLa10 (Black) - 1% Lanthanum Oxide For medium-volume terminals. Better starting and stability than WP.
- WLa15 (Gold) - 1.5% Lanthanum Oxide High-volume production. Ideal replacement for WTh20 (thoriated) without radiation.
- WLa20 (Blue) - 2% Lanthanum Oxide Intensive 24/7 production. Maximum service life and consistency in demanding applications.
Morse Tapers: History and Specifications


The Morse taper was invented in 1864 by Stephen A. Morse in New Bedford, Massachusetts, United States. Morse founded the Morse Twist Drill and Machine Company and designed this tapered holding system for drill bits. The original angle of the Morse taper is approximately 2°50' (2 degrees 50 minutes), which provides a self-centering, self-locking fit without the need for threads.
Standardization of the Morse Taper
The design was later standardized by the United States Bureau of Standards and became a worldwide industrial standard. Today it is used not only in cutting tools, but also in orthopedic medical prostheses (hip, knee) for its excellent mechanical fixation, and in resistance welding electrodes for electrical contacts.
Nomenclature: America vs Japan
In America we use the standard Morse nomenclature (Morse 1, Morse 2, Morse 3, etc.), where each number indicates a specific taper size with the characteristic angle of ~2°50'. However, some Japanese equipment manufacturers use tapers with a 1:10 ratio that have different dimensions. It is important to verify your equipment specifications to select the correct taper.
Standard Morse Sizes for Electrodes
| Morse # | Major Diameter | Minor Diameter | Length |
|---|---|---|---|
| Morse 1 | 12.065 mm | 9.045 mm | 53.98 mm |
| Morse 2 | 17.780 mm | 14.059 mm | 69.85 mm |
Note: The Morse taper size depends on the equipment design and the electrode cavity, not on the type of welding machine.
Frequently Asked Questions
Why use an insert electrode instead of a solid tungsten or molybdenum electrode?
Tungsten and molybdenum are expensive refractory materials. Only the contact face needs to be refractory — the rest of the electrode works best in copper (Class 2 CuCrZr) for heat and current conduction. An insert electrode combines a refractory tip with a copper body, delivering the same welding performance at a fraction of the cost of a solid refractory electrode.
How do I choose the right taper size for my insert electrode?
Per RWMA Bulletin 16 (Figure 18.1), taper size is determined by electrode force: #4 RW Taper (Morse 1) for up to ~600 lbs with 3/16"-5/16" face; #5 RW Taper (Morse 2) for up to ~1,000-1,200 lbs with 1/4"-5/16" face; #6 and #7 RW for higher forces. An undersized taper will loosen and slip under pressure. Some Japanese equipment uses 1:10 ratio tapers with different dimensions — verify your machine specifications.
Can I get insert electrodes with mirror finish?
Yes, but only on molybdenum (Class 14). Tungsten is too brittle and only allows improved roughness finish, not mirror. Molybdenum accepts a mirror finish by polishing, eliminating marks on silver contacts. This is the key differentiator for applications where no visible marks are acceptable on the welded component.
How long do tungsten and molybdenum insert electrodes last?
Thousands of weld points when the cooling process is maintained correctly. Electrode life depends on cooling water flow, applied force, and the workpiece material. When electrodes overheat excessively, solutions include adjusting the refractory insert length or manufacturing the entire electrode in tungsten or molybdenum for maximum temperature resistance.
What is your lead time and do you ship to the USA?
Lead time is 2 to 4 weeks when material is in stock. We manufacture in Monterrey, Mexico and ship to all of Mexico and the United States. Contact us for current availability.
What are the equivalent names for these materials from other manufacturers?
Refractory electrode materials have different trade names by manufacturer. For example: Tungsten Class 13 = CMW 100W = Tuffaloy T100W = Centerline CL-13. Molybdenum Class 14 = CMW 100M = Tuffaloy T100M = CL-14 (per RWMA Bulletin 16, Table 18.13). See our full equivalence table.